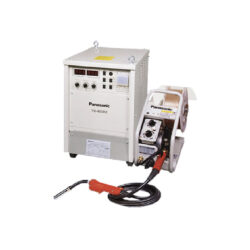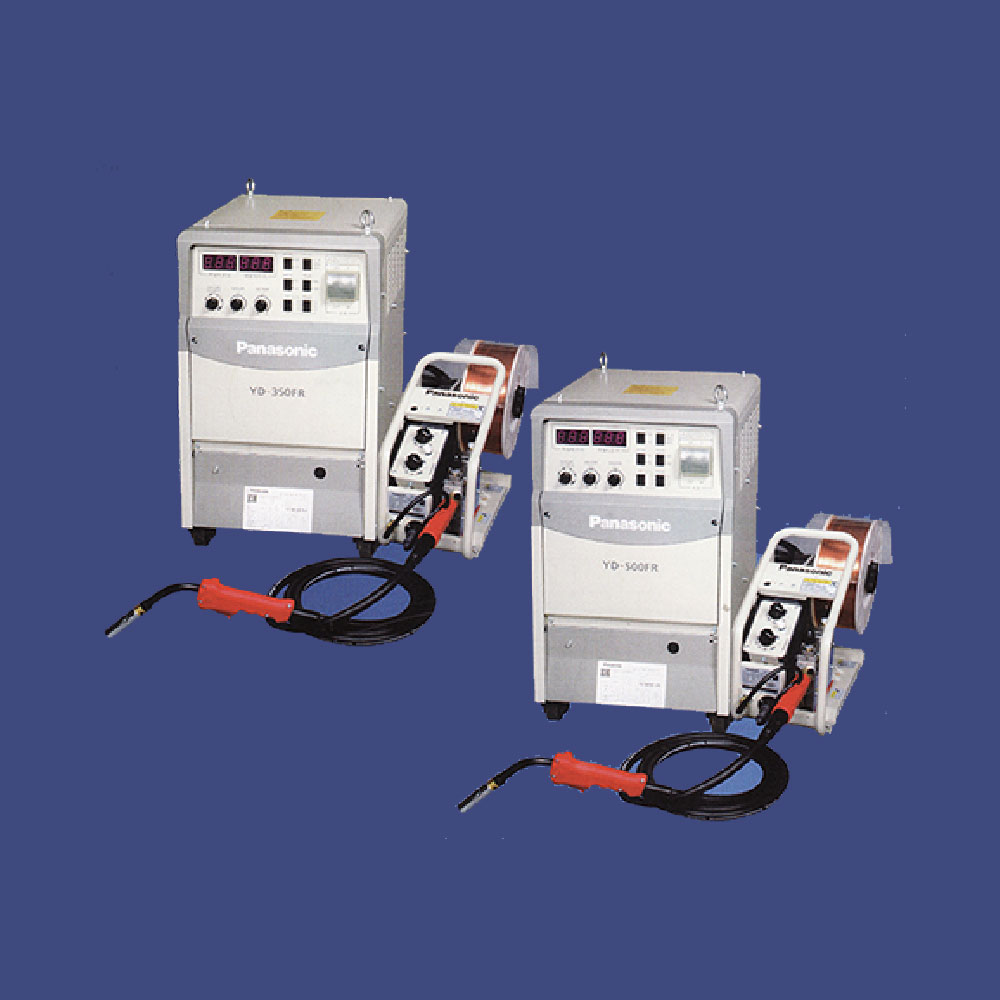
Description
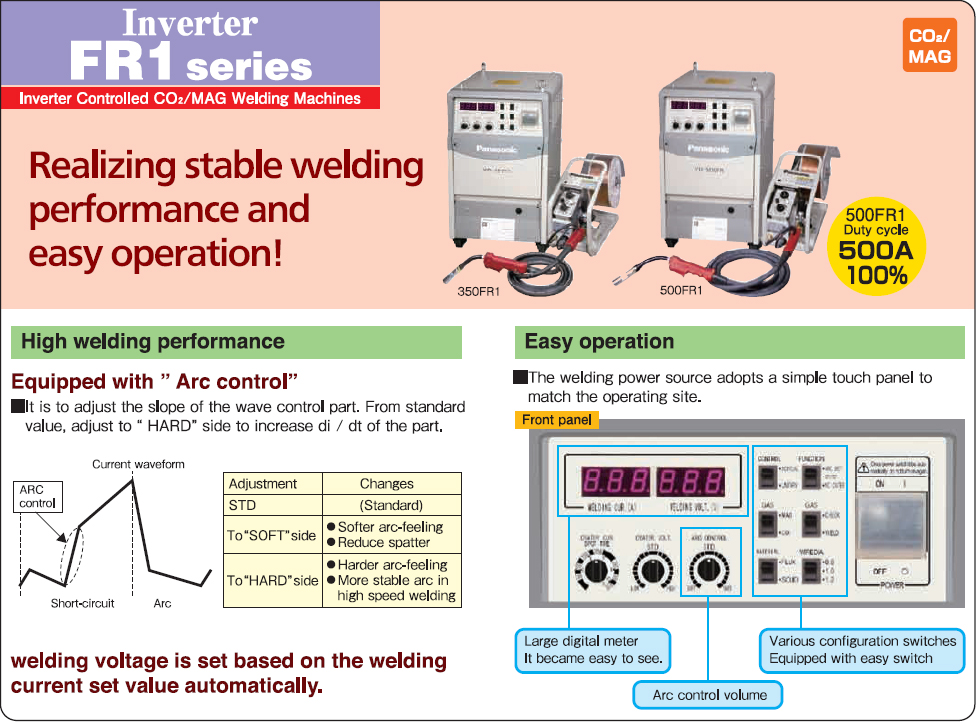
Digital control technology provide superior performance
ADVANTAGES OF 350FR1 Inverter
- Low power consumption ( 13.5kVA) at 350Amps 100% Duty Cycle
- Power saving control is equipped , the cooling fan runs a few minutes after welding operation stops
- IVF ( Panasonic patended technology ) for long distance operation with normal feeding force
- Operation is simple as KR machine
- Fine adjustment of Arc Characteristic ( both soft and hard arcs are obtainable, realizing optimum welding performance )
- Memory function , 3 programs ( reproducible storages )
- Arc spot welding available ( arc spot time – 0.3 to 10 sec )
- Compact and lightweight ( 56kg)
- Under-voltage and over voltage protections
- Over current protection
- Overheat protection
- Phase absence protection
- Management unit can expand the functions
- Limit welding current
- Lock welding parameters
- Set gas pre-flow and post-flow time
- Penetration depth control
Technical Specifications
| Specifications forYD-350FR1HGF | Specifications for YD-500FR1HGF | ||
|---|---|---|---|
| Rated input voltage | V | 415V AC ( Allowable fluctuation range:332 to 456 V) | 415 V AC (Allowable fluctuation range:332 to 456V) |
| Rated frequency | Hz | 50/60Hz(Common) | 50/60Hz (Common) |
| Number of Phase | 3-Phase | 3-Phase | |
| Rated input | kVA | 13.5 | 23.3 |
| kW | 13 | 22.4 | |
| Maximum non-load voltage | V | 70 DC | 70 DC |
| Rated output current | A | 350 DC | 500 DC |
| Rated output voltage | V | 31.5 DC | 39 DC |
| Output current adjustable range | A | 40-430 | 60-550 |
| Output voltage adjustable range | V | 16-35.5 | 17-41.5 |
| Rated duty cycle | % | 60 | 100 |
| Power control method | – | IGBT inverter type | IGBT inverter type |
| Memory | – | 3 ch, reproducible storages | 3 ch, reproducible storages |
| Applicable welding method | – | CO2, MAG | CO2, MAG |
| Waveform control method | – | Digital control:7 (small) to +7 (large) (standard:0) | Digital control:-7 (small) to + 7 ( large) ( Standard:0) |
| Sequence | – | Main welding, Main welding-Crater (“Crater repeat”is available), Arc spot | Main Welding, Main welding-Crater ( Creater repeat” is available), Arc spot |
| Applicable shielding gas | – | CO2(100% ), MAG (80% argon and 20% CO2) | CO2(100% ), MAG (80% argon and 20% CO2) |
| Applicable wire size (diameter) | mm | 0.8,1.0,1.2 | MS 1.0, 1.2, 1.6 |
| mm | MS_FCW 1.2,1.4,1.6 | ||
| Applicable wire material(Note) | – | Mild steel (MS) Flux cored mild steel (MS_FCW) ( Only for 1.2mm) | Mild steel (MS) Flux cored mild steel ( MS_FCW) |
| Gas purge time | – | 1 second-1 minute / continuous | 1 second-1 minute/continuous |
| Pre-flow time | s | 0.2s | 0.2s |
| post-flow time | s | 0.2s | 0.2s |
| Arc spot time | s | 0.3-10.0 ( Increment of 0.1) continuous | 0.3-10.0 ( Increment of 0.1) continuous |
| Input power terminal | – | Terminal block (for 3-phase, M5 bolting) | Terminal block ( for-3-phase, M5 bolting) |
| Output terminal | – | Copper terminal with M8 bolting | Copper terminal with M8 bolting |
| Dimension ( Width x Depth x Height) | mm | 372X545X669 | 372X545X669 |
| Mass | kg. | 56 | 62 |